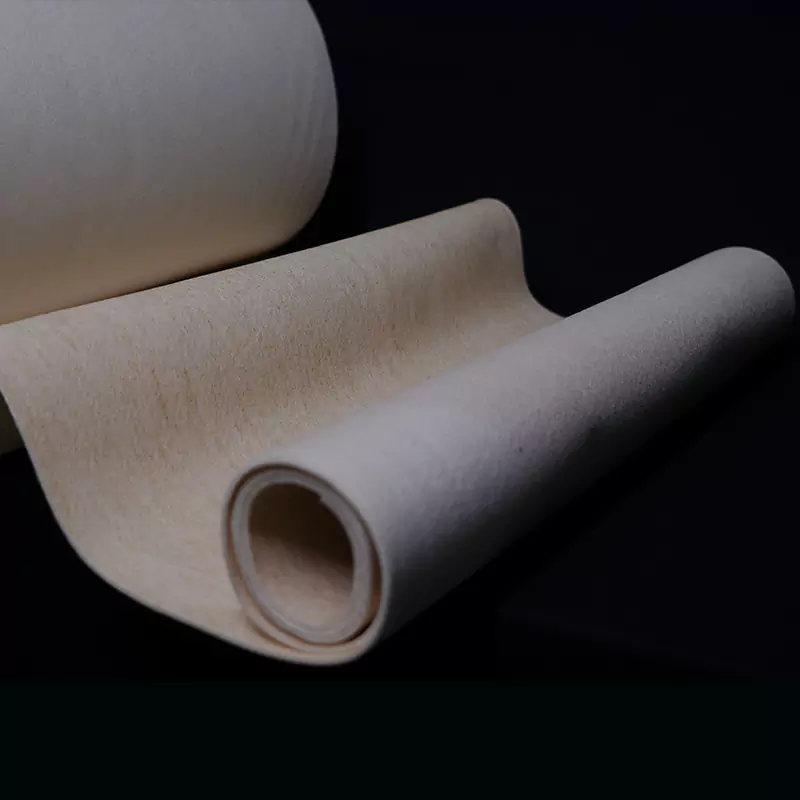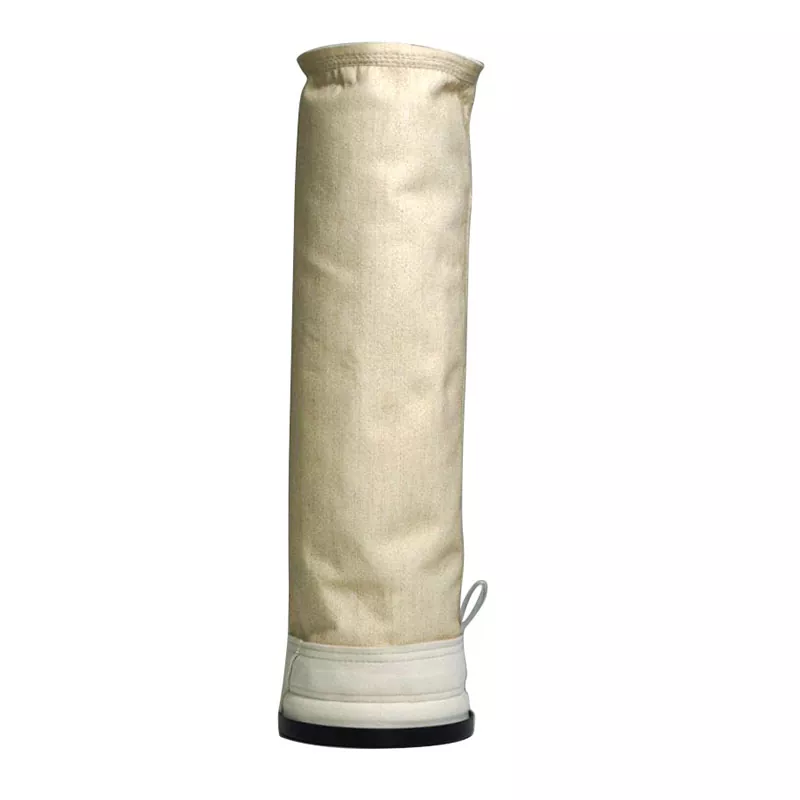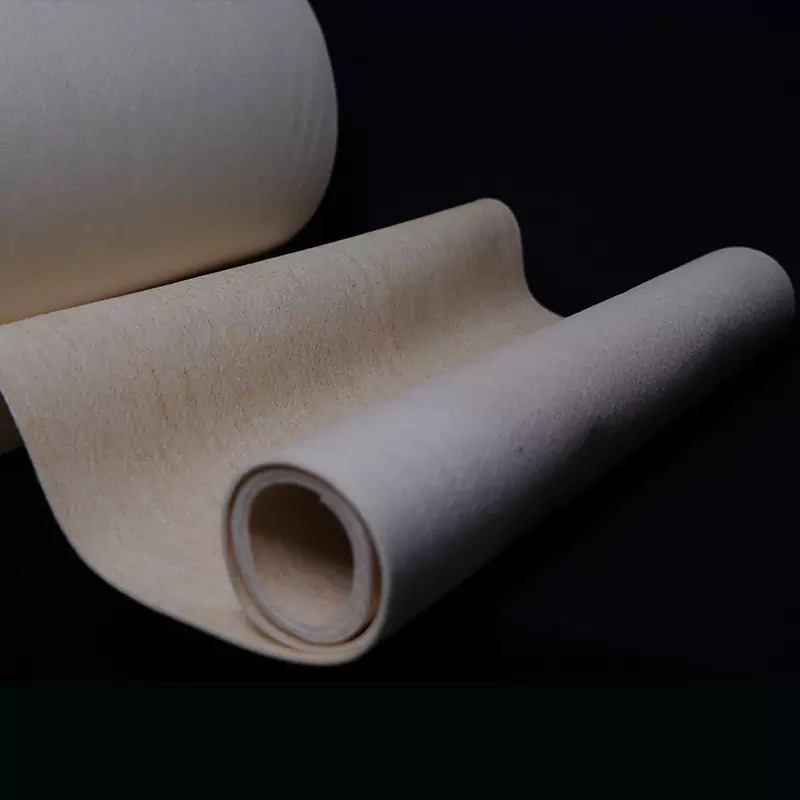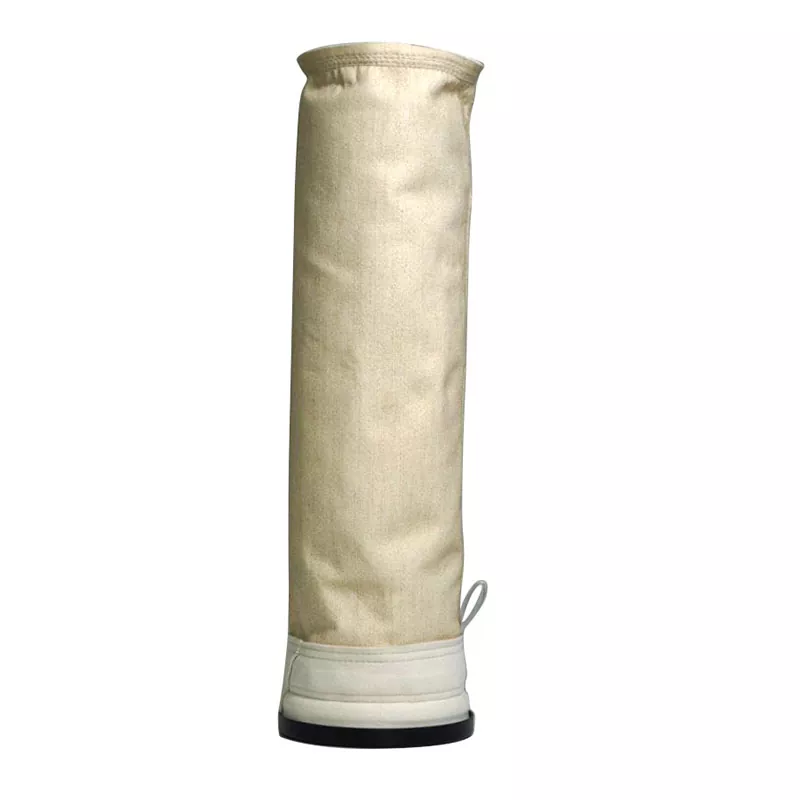
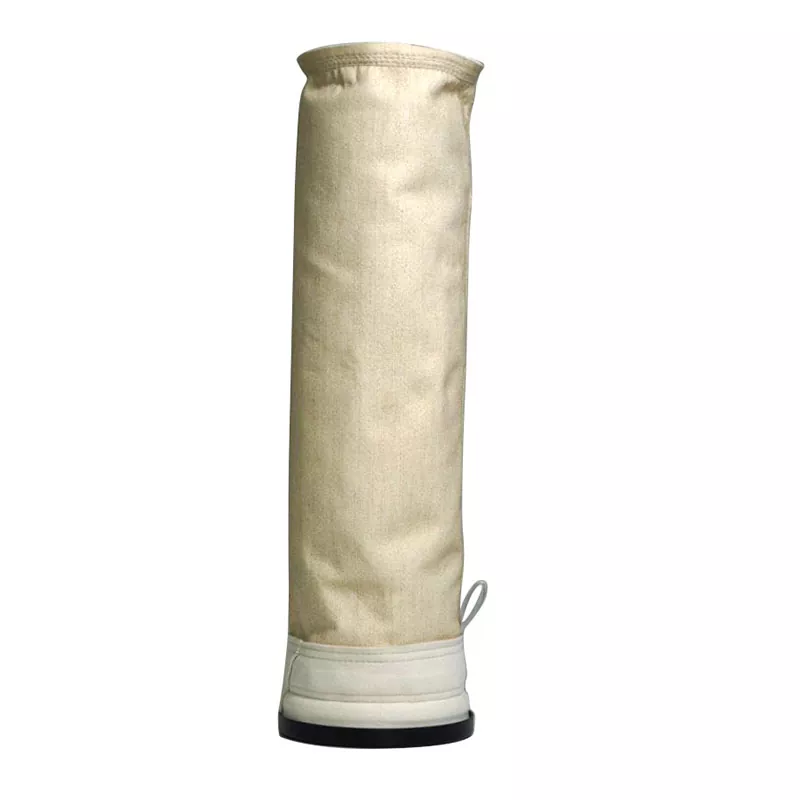
The cement plant filter bags produced by FST are precision engineering filtration solutions designed specifically for the harsh operating conditions of cement manufacturing. They combine extreme temperature resistance, wear resistance, and high dust removal efficiency to minimize downtime for replacing filter bags and reduce energy consumption. They are suitable for new cement plants and retrofitting existing system applications.
Excellent filtration efficiency: filtration efficiency of Cement Plant Filter Bags can reach 99.99%
Chemical resistance: acid and alkali resistant flue gas (pH 3-11), moisture, and chemical byproducts of cement combustion (sulfates, chlorides)
·Cement kiln: Preheater, pre decomposition furnace, and kiln inlet/outlet dust collection (processing high temperature and grinding kiln dust)
·Raw material processing: crusher, conveyor belt, silo ventilation and dust removal
·Burning system: purification of flue gas at the rotary kiln head and tail
·Grinding system: cement mill, coal mill, vertical grinding powder dust collection
·Finished product processing: powder selection machine, warehouse top, warehouse bottom, packaging system dust removal
·Auxiliary processes: Drying machine, cooling machine, settling chamber dust control
FST focuses on the research and production of filter bags for cement plants. Our cement plant filter bags have unparalleled performance. Welcome to contact and negotiate!
We are committed to partnering with you to meet your unique filtration needs—let’s build a cleaner, more efficient cement production process together!
Address
No. 8 Zeyuan Road, Jiuyuan District, Baotou City, Inner Mongolia Autonomous Region, China
Tel